5083 Marine Grade Aluminum

 For workboats, ferries, fishing vessels, offshore structures, and deck equipment, 5083 marine grade aluminum is valued for high strength without sacrificing seawater corrosion resistance. The material's most important purchasing concern is not simply nominal chemistry. It is whether the supplied temper, welding practice, and inspection records will control corrosion around welds during service.

This alloy belongs to the non-heat-treatable 5xxx aluminum family. Its strength is obtained primarily through magnesium alloying and strain hardening, rather than precipitation heat treatment. That makes it practical for fabricated marine structures, but it also means weld heat can reduce strength in the heat-affected zone.
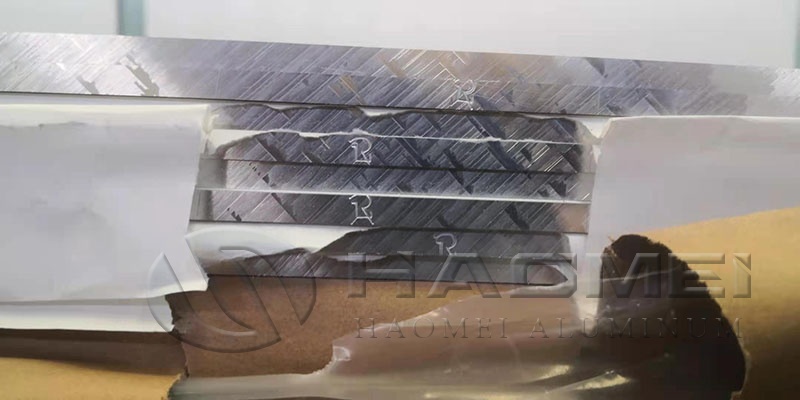
marine aluminum plate

Why It Matters

A vessel hull can use compliant material and still develop avoidable problems if welding, storage, or material traceability are poorly controlled. The highest-risk locations are often:

  • Continuous weld seams exposed to salt spray.

  • Deck-to-bulwark joints that retain standing water.

  • Areas with dissimilar-metal fasteners.

  • Welded panels operating at elevated temperature for extended periods.

  • Crevices beneath fittings, insulation, or non-draining supports.

The practical objective is to maintain corrosion resistance while accounting for lower post-weld mechanical properties. Material selection should therefore be reviewed alongside fabrication drawings and welding procedure specifications.

Alloy Data

ASTM B209/B209M identifies 5083 as an aluminum-magnesium alloy containing 4.0% to 4.9% magnesium, 0.4% to 1.0% manganese, and 0.05% to 0.25% chromium by weight. These limits should be verified against the mill test certificate for each production batch.

PropertyTypical Requirement or ReferencePurchasing Relevance
Alloy familyAluminum-magnesium, 5xxx seriesGood natural resistance in marine atmospheres
DensityApproximately 2.66 g/cm³Supports vessel weight reduction calculations
Common marine tempersO, H116, H321H116 and H321 are commonly specified for marine service
Main fabrication issueHeat-affected-zone softeningDesign weld regions using post-weld values
Corrosion concernSensitization and exfoliation riskRequires controlled temperature exposure and verified temper

ASTM B928/B928M covers high-magnesium aluminum alloy products in H116 and H321 tempers intended for marine service and similar environments. It includes additional requirements associated with exfoliation-corrosion resistance. When a specification calls for marine material, referencing only the alloy number is incomplete. State the product standard and required temper.

For structural applications, request 5083 aluminum plate with clear thickness tolerances, temper, ultrasonic testing requirements where applicable, and mill certificates tied to the delivered identification marks.

Temper Choice

Temper selection changes both fabrication behavior and corrosion assurance.

TemperBest FitImportant Check
ODeep forming, complex curved partsLower strength than strain-hardened tempers
H116Hull plating and structures exposed to seawaterConfirm ASTM B928/B928M compliance when specified
H321Marine structures requiring stabilized strain-hardened materialReview corrosion-test documentation and service temperature

H116 and H321 are not interchangeable merely because both are marine-associated tempers. Confirm the exact condition required by the vessel design, classification rules, and applicable contract specification.

For higher-strength alternatives in certain welded structures, 5383 aluminum plate may be evaluated by the engineering team. Substitution should never be made based on strength alone because weldability, forming limits, corrosion behavior, and approval requirements can differ.

Welding Controls

5083 is commonly welded with gas metal arc welding or gas tungsten arc welding. Filler selection should follow the qualified welding procedure rather than a generic preference. AWS A5.10/A5.10M covers aluminum and aluminum-alloy welding electrodes and rods, including commonly specified ER5183 and ER5356 filler classifications.

Use this fabrication checklist before production welding:

  1. Remove moisture, oil, oxide, paint, and salt contamination from joint edges.

  2. Segregate aluminum-only brushes and grinding tools to prevent iron contamination.

  3. Qualify welding procedure specifications using the actual base-metal temper and thickness range.

  4. Limit unnecessary heat input and repeated repair cycles.

  5. Design weld access to avoid incomplete fusion, crevices, and water traps.

  6. Record filler classification, shielding gas, welding parameters, and welder qualification.

  7. Inspect critical seams using the non-destructive examination method required by the project.

Welding softens strain-hardened material adjacent to the weld. Structural calculations must use approved post-weld allowable properties, not parent-metal certificate values alone. This is especially important for high-load brackets, longitudinals, crane foundations, and pressure-containing assemblies.
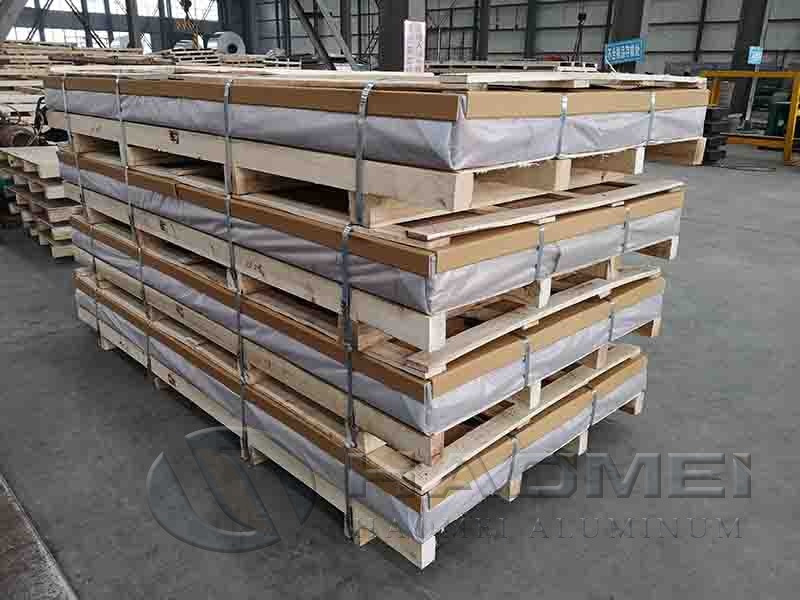
aluminum sheet stock

Corrosion Tests

The phrase marine grade does not mean the alloy is immune to every corrosion mechanism. High-magnesium 5xxx alloys can become sensitized after prolonged exposure to elevated temperatures, which may increase susceptibility to intergranular or exfoliation corrosion.

ASTM G66, commonly called the ASSET test, is used to evaluate exfoliation-corrosion susceptibility in 5xxx series aluminum alloys. ASTM B928/B928M references corrosion-performance requirements for qualifying H116 and H321 material. Request test evidence when the application involves prolonged warm service, high salinity, or critical safety structures.

Ask suppliers to provide:

  • Mill test certificate with heat number and chemical analysis.

  • Temper and governing material standard.

  • Corrosion-test documentation when required by specification.

  • Mechanical test results for the applicable thickness range.

  • Traceable packing labels matched to certificate records.

  • Surface condition statement, including protective film or paper where needed.

Cost Checks

Quoted material price should be compared on a like-for-like basis. A lower initial figure can omit testing, traceability, protective packing, dimensional control, or certification needed for marine construction.

Cost ItemQuestion to AskRisk if Omitted
TemperIs H116 or H321 stated on the quotation?Incorrect corrosion or strength performance
StandardDoes the offer cite ASTM B928/B928M or project standard?Ambiguous marine-service suitability
CertificateIs the heat number traceable to the certificate?Material cannot be verified at inspection
CuttingAre edge condition and dimensional tolerances defined?Extra machining and welding preparation
PackingIs protection suitable for salt-air transport?Staining and surface damage before fabrication

A technically complete purchase specification should state alloy, temper, standard, dimensions, tolerances, required documentation, corrosion-test requirement, inspection scope, and packing method. This approach protects welded marine structures from preventable corrosion issues before fabrication begins.

Original source: https://www.marine-aluminium-plate.com/a/5083-marine-grade-aluminum.html
Aluminium Strip 25mm X 3mm Price

 Pricing for a 25mm x 3mm aluminium flat product can look simple until two quotations show very different totals. During the last three months, the following questions have appeared repeatedly in English-language search and Q&A discussions from people comparing stock sizes, alloys, and delivery costs. The answers focus on the commercial details that can change the final amount.

flat aluminum strip

1. What is the aluminium strip 25mm x 3mm price per metre?

There is no universal per-metre price because suppliers may quote different alloys, tempers, edge conditions, and order quantities. A practical starting point is the material weight.

A 25mm x 3mm section has an area of 75mm2. Using aluminium density of approximately 2,700kg/m3, it weighs about 0.203kg per metre. A 6m length therefore weighs roughly 1.215kg before packaging allowance.

DimensionApproximate WeightTypical Use in Calculations
25mm x 3mm x 1m0.203kgComparing a per-metre quotation
25mm x 3mm x 3m0.608kgSmall workshop or fabrication requirement
25mm x 3mm x 6m1.215kgStandard long-length requirement

To estimate the material portion, multiply the weight by the quoted price per kilogram. Then add cutting, protective film, surface treatment, packing, freight, taxes, and any minimum order charge. A low metal rate can become less competitive when short-length cutting or express delivery is included.

2. Why do 1050, 1060, 3003, and 5052 quotations differ for the same size?

The dimensions may match, but alloy chemistry and mechanical performance do not. Pure or near-pure grades such as 1050 and 1060 are valued for conductivity, formability, and corrosion resistance. They are often selected for electrical, decorative, and general fabrication work. For routine soft-temper requirements, a 1050 Aluminium Metal Strip can be a sensible option.

3003 includes manganese and generally offers higher strength than 1000-series material. It is common where moderate forming ability and improved durability are needed. 5052 contains magnesium, giving it stronger corrosion resistance and better strength for many marine, transport, and damp-environment applications. A 5052 Aluminum Strip quotation can therefore be higher than a 1050 option, particularly in a hard temper.

AlloyRelative Cost TendencyMain Commercial Reason
1050 / 1060Often lowerHigh aluminium purity and broad availability
3003ModerateManganese alloying and stronger properties
5052Often higherMagnesium alloying and corrosion performance
6061Variable to higherHeat-treatment requirements and strength

Do not choose solely by the lowest rate. State the intended application, whether the material will be bent, drilled, welded, polished, or used for electrical contact. This prevents paying for an unnecessary grade or receiving one that is too soft for the job.

aluminum strip stock

3. Is 25mm x 3mm aluminium sold as rolled material or flat bar?

This is one of the most important questions because the same nominal dimensions can describe different production routes. A narrow rolled product is typically slit from wider material and may have mill edges or deburred slit edges. Flat bar is commonly extruded, then supplied in straight lengths with different corner radii, flatness, and dimensional tolerances.

Ask the supplier to confirm all of the following:

  • Production method: rolled or extruded.
  • Edge condition: mill edge, slit edge, deburred edge, or rounded edge.
  • Temper: for example, O, H14, H24, T4, or T6.
  • Width and thickness tolerances.
  • Straightness and flatness requirement.
  • Length supplied and cutting tolerance.

For decorative trim, electrical connectors, and bending operations, edge quality can matter as much as alloy. For structural brackets, temper and straightness frequently matter more. A quotation that only says "25 x 3 aluminium" leaves too much room for an unsuitable substitution.

4. How much do cutting, anodising, and colour coating add to the price?

Secondary processing can represent a large share of the delivered value, especially on small quantities. Cutting a 6m length into many short pieces adds machine time, handling, and scrap. Tight cut tolerances usually add another charge. Anodising, powder coating, or painted finishes depend on colour, coating thickness, surface preparation, and minimum processing batch size.

Added RequirementEffect on Quoted AmountDetail to Specify
Cut-to-length piecesUsually increases itPiece length, quantity, and cut tolerance
Deburred edgesUsually increases itOne edge or all edges, acceptable burr level
Clear anodisingIncreases itFinish grade and film thickness
Black or coloured coatingIncreases itColour reference, gloss, coating thickness
Protective filmSmall added costOne-side or two-side protection

If appearance is critical, request a sample or written finish description before production. A polished surface, brushed surface, and standard mill finish can look significantly different even when the alloy and dimensions are identical.

5. What should I include when requesting a reliable 25mm x 3mm aluminium quotation?

A complete enquiry reduces back-and-forth and makes competing offers easier to compare. Give the exact alloy, temper, dimensions, total quantity, length, and finish. Also state whether the quoted amount should include packing and delivery to your location.

A useful enquiry format is: "Please quote aluminium 25mm x 3mm, alloy 5052-H32, 3m lengths, 200 pieces, deburred slit edges, mill finish, packed for road transport, delivery included to . Please state unit weight, tolerance, lead time, certificate availability, and payment terms."

For an accurate comparison, check whether each offer includes the same items. One supplier may quote net material weight only, while another may include cutting, export packing, and freight. Confirm currency, Incoterm, validity period, production lead time, and whether a material test certificate is available. These details make the stated aluminium strip 25mm x 3mm price meaningful rather than merely attractive at first glance.

1060 aluminum strip

Original source: https://www.aluminumstrip24.com/news/aluminium-strip-25mm-x-3mm-price.html

5754 and 5083 Aluminum Plate For Fuel Tanker Trailer

 In the manufacturing of tanker trailers, the material used for the tank body not only influences the vehicle's tare weight and transport efficiency but also directly affects its corrosion resistance, weld quality, service life, and safety. With the industry's shift toward lightweight transport equipment, aluminum alloy tank semi-trailers—prized for their low weight, high payload capacity, and excellent corrosion resistance—have increasingly become a preferred choice for transporting refined petroleum products, liquid chemicals, and certain types of hazardous materials.

Among the materials used, 5083 and 5754 aluminum plates are the most common aluminum-magnesium alloys employed in the construction of these tank trailers.

5754 and 5083 Aluminum Plate For Fuel Tanker Trailer.jpg

5083 Aluminum Alloy: A Key Material for Tank Bodies

5083aluminum plate is an Al-Mg (aluminum-magnesium) alloy with a high magnesium content. It offers high strength, superior corrosion resistance, and excellent weldability, making it particularly well-suited for transport equipment frequently exposed to humid conditions, salt spray, petroleum products, and complex outdoor environments. In the context of tank semi-trailers, 5083 aluminum is commonly used for tank shells, end caps (heads), internal baffles, and various load-bearing structural components.

Because tank bodies must withstand liquid pressure, vibrations during transit, impact forces during loading and unloading, and long-term fatigue, the materials used must possess high strength and maintain stability after welding.

5083 aluminum retains excellent overall performance following welding and is well-suited for processes such as TIG (argon arc) welding and MIG welding. Its outstanding resistance to seawater and industrial atmospheric corrosion also makes it an exceptional choice for use in coastal regions, high-humidity areas, and chemical transport applications.

Common tempers of 5083 aluminum used for tank semi-trailers include:

5083-H111: This temper features a degree of strain hardening while retaining good formability and weldability. It is typically used for tank shells and end caps that require processes such as rolling, pressing, and welding.

5083-H116: This temper offers superior strength and corrosion resistance, making it especially suitable for tank shells, internal baffles, and external structural components that demand high resistance to corrosion.

5083-H321 Aluminum Plate: Subjected to a stabilization treatment, this alloy offers excellent resistance to stress-corrosion cracking and superior dimensional stability. It is well-suited for tank components that require high fatigue resistance and long-term operational stability.

When selecting materials, the thickness of the tank plating is typically determined by considering factors such as tank capacity, the medium being transported, design pressure, the vehicle's gross weight, and relevant industry standards. For large tanker semi-trailers, aluminum plates in the 5083-H111, H116, or H321 tempers are frequently chosen for the main tank body.

5754 Aluminum Plate: Balancing Formability and Corrosion Resistance

Also belonging to the Al-Mg (aluminum-magnesium) series of corrosion-resistant alloys, 5754 aluminum plate generally has a lower strength than 5083, but it offers superior plasticity, stampability, and ease of processing. 5754 exhibits excellent corrosion resistance, maintaining stable performance during the transport of standard petroleum products, as well as in humid environments and outdoor conditions.

In the manufacturing of tanker semi-trailers, 5754 aluminum is often used for non-primary load-bearing components, such as toolboxes, walkways, protective panels, mudguards, side guards, edge trim, lightweight hatches, piping covers, and various interior or auxiliary structural parts. It is particularly advantageous for components that require bending, stamping, deep drawing, or roll-forming.

Common tempers for 5754 aluminum plates used in tanker semi-trailers include:

5754-H111: Suitable for general bending, rolling, and welding; often used for auxiliary enclosures, protective guards, and certain lightweight structural components.

5754-H22: Features a moderate degree of work hardening, offering a balance between strength and formability; ideal for covers and protective components that require a specific level of structural rigidity. 5754-H32 aluminum sheet: Offers relatively higher strength while maintaining good workability; commonly used for walkways, protective panels, enclosure panels, and components that require a certain degree of resistance to deformation.

5754-O temper aluminum sheet: In an annealed state, it exhibits excellent plasticity, making it suitable for deep drawing, complex bending, or the fabrication of parts that require high formability.

How to choose between 5083 and 5754?

In short, 5083 aluminum sheet is better suited for the primary load-bearing and pressure-bearing structures of tanker semi-trailers—such as the tank body, tank heads, and internal baffles—whereas 5754 aluminum plate is more appropriate for auxiliary structures, exterior cladding, and components that demand superior formability. Using a combination of both allows for vehicle lightweighting and optimized manufacturing costs, all while ensuring safety and durability.

When procuring aluminum sheets for tanker trailers, beyond the alloy grade, it is essential to verify the material temper, thickness tolerances, flatness, surface quality, mechanical properties, ultrasonic testing requirements, and relevant quality certification documentation.

For tankers designed to transport gasoline, diesel, aviation kerosene, or chemical liquids, the appropriate material temper must be selected based on the specific characteristics of the transported medium, tank design specifications, and manufacturing processes.


Original Source:https://www.aluminumtankerplate.com/a/5754-and-5083-aluminum-plate-for-fuel-tanker-trailer.html

Aluminum Sheet Circle Specifications for Low-Defect Deep Drawing

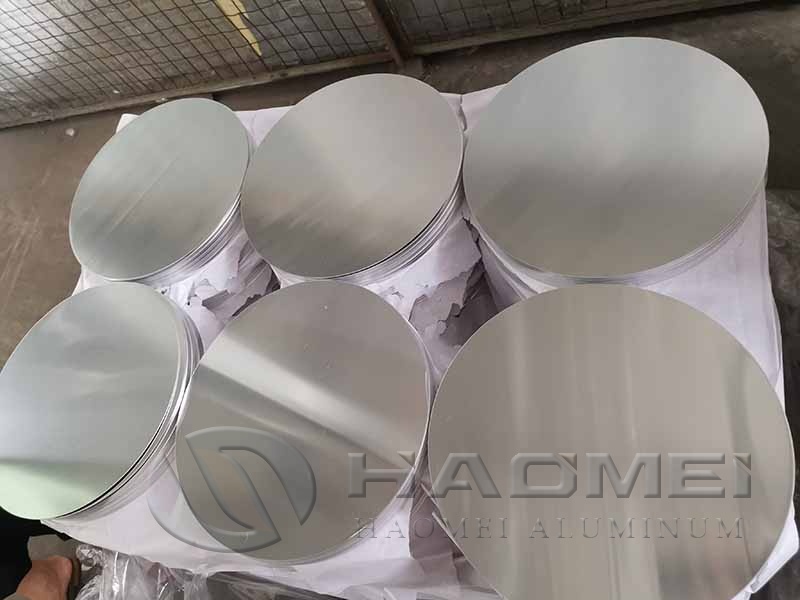
 For cookware, lighting, pressure vessels, and spun components, the highest-cost issue is often not the metal price. It is forming scrap caused by cracking, earing, wrinkling, or burr-related tool damage. A properly specified aluminum sheet circle helps reduce these defects before press production begins.

The most important product feature for deep drawing is stable formability, which depends on alloy, temper, thickness consistency, grain structure, surface condition, and cut-edge quality. Diameter alone is not enough for a usable round blank.

aluminum circle for cookware

1. Match Alloy and Temper to the Forming Operation

Aluminum circles are commonly produced from non-heat-treatable wrought alloys. For drawn cookware and general stamping, 1xxx and 3xxx series materials are frequently considered because they offer useful ductility and corrosion resistance.

ApplicationCommon Alloy FamiliesTypical Temper DirectionMain Requirement
Deep-drawn cookware1050, 1060, 1070O temperHigh elongation and low cracking risk
Cookware with higher strength needs3003O temperBetter strength than 1xxx with workable formability
Lighting reflectors1050, 1060, 1100H14 or application-specificSurface consistency and controlled forming
Spinning and shallow forming1050, 1060, 3003O, H12, H14Stable thickness and smooth edges

For deep drawing, O temper is generally selected when maximum ductility is needed. A harder temper can improve handling stiffness, but it may increase the likelihood of splits in high draw-ratio parts.

Ask the mill or converter to identify the applicable standard on the quotation and certificate. ASTM B209 covers aluminum and aluminum-alloy sheet and plate, while EN 485-2 specifies mechanical-property requirements for wrought aluminum sheet, strip, and plate. If circles are cut from parent material, the agreed blank tolerances should be stated separately because final diameter and edge condition are process-dependent.

A suitable Aluminum Sheet Circle specification should state the intended process, such as deep drawing, spinning, stamping, or anodizing. This prevents a general-purpose blank from being supplied for a demanding forming operation.

2. Control Flatness, Thickness, and Burr Before Pressing

A round blank can look acceptable in a stack yet create repeated press failures. Thickness variation changes material flow. Excessive burrs can scratch tooling, interfere with stacking, and initiate cracks at the blank edge.

Use this acceptance checklist in purchase documentation:

Control PointWhat to SpecifyWhy It Matters
DiameterNominal diameter and permitted toleranceSupports repeatable tool clearance and draw results
ThicknessNominal thickness and tolerance rangeReduces uneven wall thickness after drawing
TemperAlloy and temper, such as 1050-O or 3003-ODefines expected forming response
FlatnessMaximum allowable wave, buckle, or dish conditionHelps automatic feeding and blank seating
Edge conditionDeburred, no sharp edge, maximum burr height if requiredProtects dies and improves safe handling
SurfaceMill finish, oiled or dry, scratch and stain limitsSupports coating, polishing, and appearance needs
Grain directionState if earing performance is criticalHelps control rim variation after drawing

Thickness should be verified with calibrated micrometers at multiple points around the blank, not only at its center. Diameter can be checked with a suitable caliper, optical system, or go/no-go gauge depending on the tolerance requirement.

For high-volume drawn products, request first-article samples from the production blanking route. Test them with the actual die set, lubricant, and draw depth. Material performance in a laboratory tensile test does not always predict behavior in a specific press tool.

aluminum circle stock

3. Prevent Earing and Cracking With a Practical Qualification Plan

Earing is the wavy rim that appears after drawing. It is linked to planar anisotropy in rolled material, meaning the metal deforms differently at different directions relative to the rolling direction. Severe earing increases trimming loss and can make rim-height control difficult.

Before approving production material, use a staged qualification plan:

  1. Define the finished part dimensions, draw depth, wall-thickness target, and allowed trimming loss.

  2. Select an alloy-temper combination based on the forming severity, not only the lowest starting price.

  3. Obtain samples from the same production route proposed for regular supply.

  4. Conduct trial draws with production tooling and the planned lubricant.

  5. Record crack location, rim height variation, surface scratches, and wall thinning.

  6. Agree on lot traceability and retain samples for comparison if future variation occurs.

For cookware intended to contact food, do not assume that a generic alloy statement is sufficient. Food-contact obligations vary by sales region and by the full finished article, including coatings, pigments, adhesives, and cleaning instructions. Request material traceability and any relevant declarations needed for the destination market. In the United States, food-contact requirements are administered by the U.S. Food and Drug Administration; in the European Union, framework requirements include Regulation (EC) No 1935/2004.

Price comparisons should separate the metal reference from conversion costs. A transparent quotation often uses an aluminum market reference, such as the London Metal Exchange cash price, plus an agreed premium, rolling conversion, blanking charge, packaging, and freight. Comparing only price per kilogram can hide differences in thickness tolerance, inspection level, and usable yield.

For programs requiring consistent cookware blanks, Aluminum Circles should be ordered with documented alloy, temper, dimensional tolerances, edge requirements, packing method, and inspection records. This turns forming quality from an assumption into a measurable supply requirement.

large round aluminum sheet

A complete request should include: alloy and temper, diameter, thickness, tolerance limits, application, forming method, surface expectation, burr limit, packaging quantity, destination, and required certificates. These details allow suppliers to assess whether the proposed blank is suitable for the actual production process rather than merely meeting a nominal size.

Original source: https://www.hm-alu.com/a/aluminum-sheet-circle.html

5083 Marine Grade Aluminum

  For workboats, ferries, fishing vessels, offshore structures, and deck equipment, 5083 marine grade aluminum is valued for high strength w...